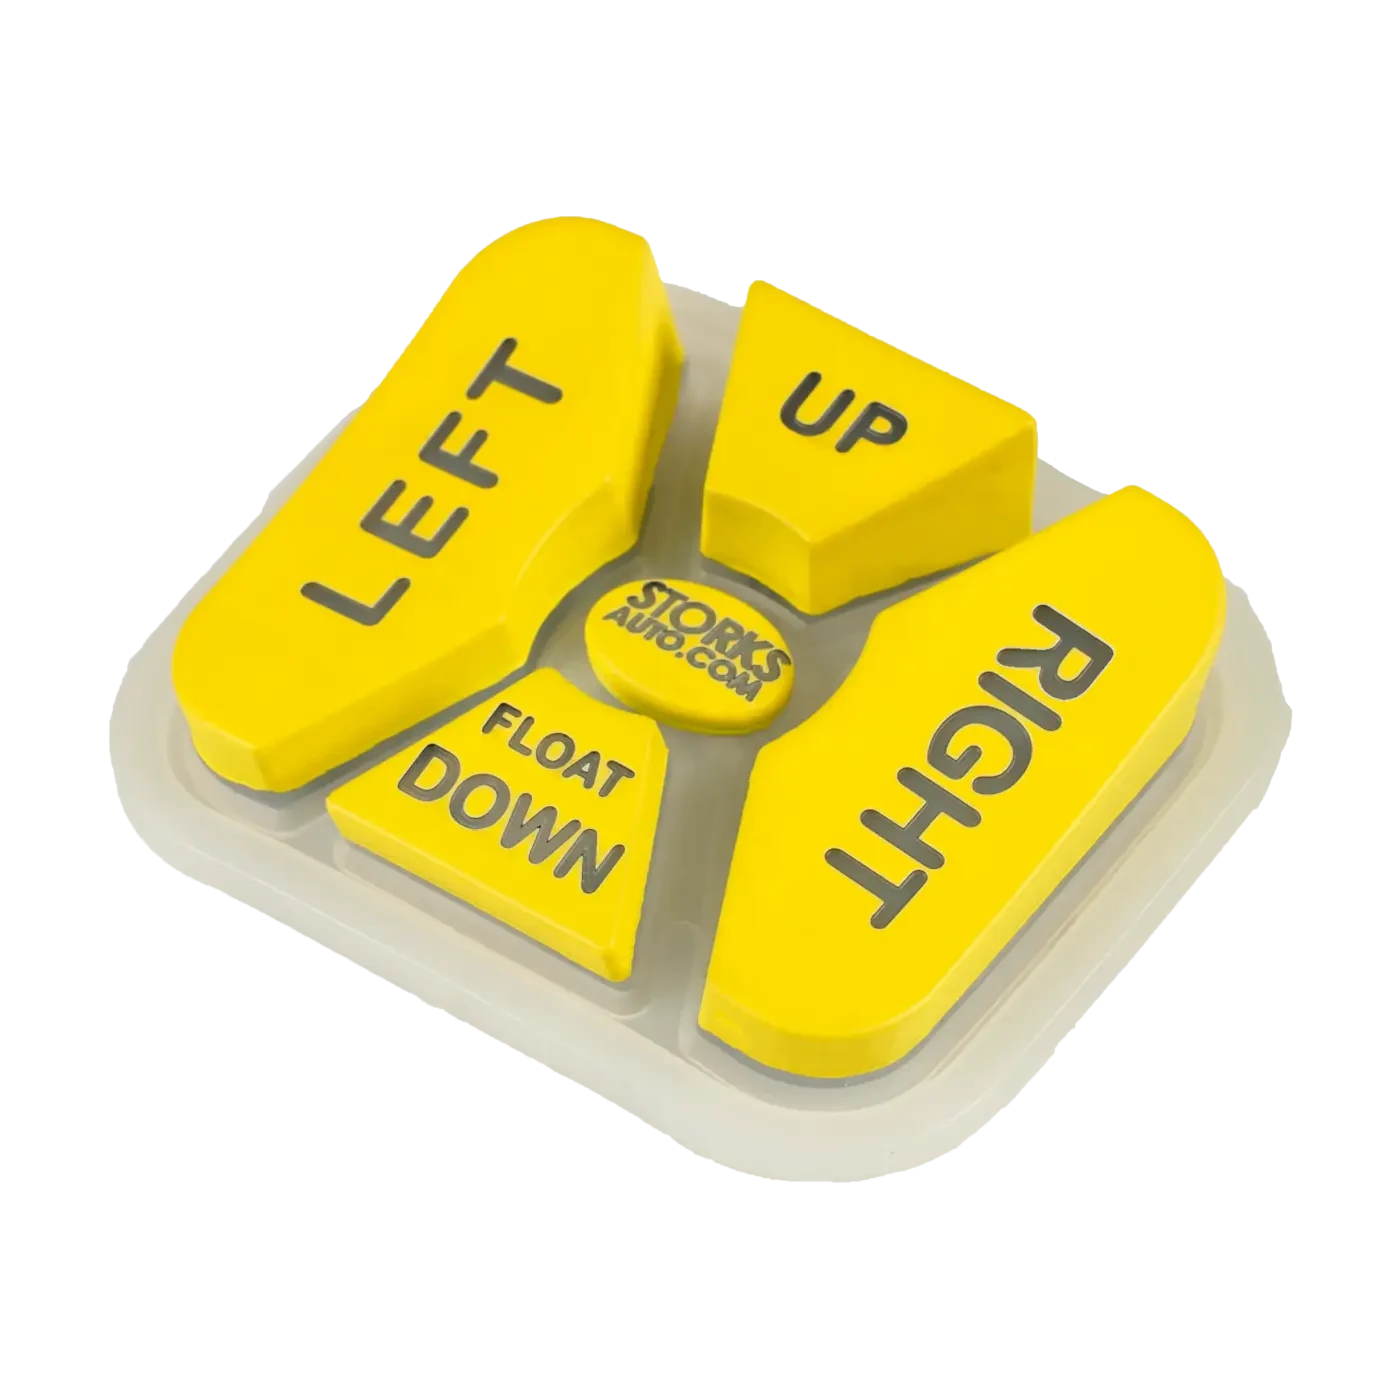
Compression molding and LSR injection can both produce silicone keypads, but they describe different material-and-process combinations. Liquid silicone rubber (LSR) is a material family, while liquid injection molding is a processing route commonly used for LSR. High-consistency rubber (HCR) is widely used in compression and transfer molding, but HCR can also be injection molded. The right route therefore depends on the compound, tool concept, key geometry, contacts or inserts, secondary operations, production plan, and validation method—not on annual volume alone.
For buyers comparing quotations, the useful question is not simply “Which process is better?” It is: Which route can repeatedly make this keypad with the required feel, contact function, appearance, assembly interfaces, and inspection evidence?
For broader keypad architecture, see JASPER’s silicone rubber keypad design guide. For mold release and first-article controls, use the silicone keypad tooling and prototyping guide.
- Distinguish Material Form from Molding Process
- Compare the Process Routes Before Comparing Price
- Engineering Selection Matrix
- Compare Tooling and Part Geometry Needs
- Review Contacts, Colors, and Secondary Operations
- Evaluate Capacity and Quality Controls
- Validate the Keypad, Not Just the Molding Process
- Select a Route with the Manufacturing Partner
Distinguish Material Form from Molding Process
Silicone sourcing becomes confusing when material names and process names are treated as synonyms.
LSR is a pumpable two-component silicone system. Its components are mixed and heat-cured, and liquid injection molding is one processing route. This flowable material behavior distinguishes LSR from higher-viscosity HCR.
HCR is a higher-viscosity silicone family. Suitable formulations can be processed by injection, compression or transfer molding; HCR is not restricted to compression and transfer routes.
That distinction matters because a drawing that says only “silicone rubber” does not define how the material will be fed, filled, cured, demolded, trimmed, or inspected. A useful RFQ should therefore identify the proposed material family, molding route, contact or insert method, color/finish sequence, and production controls separately.
Compare the Process Routes Before Comparing Price
Compression molding places a prepared quantity of silicone in an open mold. Closing the mold applies pressure to move material through the cavity; the rubber cures and the part is demolded. This is a common HCR processing route.
LSR injection meters and mixes liquid components before injecting them into a heated mold. Industrial configurations can include dedicated dosing, LSR nozzles, cold runners and mold vacuum. The process can support short cycles and substantial automation when the material, tool and equipment are suitably configured.
Those capabilities can change the economics, but they do not create a universal rule. Compression molding may be attractive when the tool, loading method, inserts, secondary operations, and lot pattern fit a direct molding route. LSR injection may be attractive when a stable design benefits from closed-mold filling, multi-cavity tooling, controlled dosing, or automated handling. Insert loading, color changes, coating, laser processing, trimming, inspection, maintenance, and demand variability can change the result.
Engineering Selection Matrix
| Decision factor | Compression-molding direction | LSR-injection direction | What the OEM should confirm |
|---|---|---|---|
| Material | Commonly HCR/prepared charge | Commonly two-component LSR | Exact material family, approved grade, cure/post-cure responsibility |
| Tooling | Charge placement and closing flow matter | Gate, runner/nozzle, dosing and cavity filling matter | Parting line, feed/gate, venting, flash, demolding |
| Geometry | Suitable for many keypad geometries; charge flow still matters | Flowable material can support intricate or thin features with suitable tooling | Thin webs, tall walls, shutoffs, trapped-air zones, key-to-key balance |
| Contacts/inserts | Preformed contacts or inserts may be loaded before molding | Inserts or multi-component concepts are possible but can reduce automation benefits | Loading method, position control, contamination, retention, inspection |
| Color/finish | Molded color plus secondary print/coating/laser as required | Molded color plus secondary print/coating/laser as required | Number of colors, changeover, boundary quality, downstream operations |
| Automation | Manual or semi-automated routes are common, but project-specific | Often offers stronger automation potential | What automation is actually included in the quoted route |
| Volume/economics | Can support development and repeat production | Can suit stable repeat production when tool/process investment is justified | Tool cost, cavity count, labor, cycle, scrap, finishing, inspection, lot size |
| Quality control | Charge, cure, cavity, flash, trim and insert controls may matter | Dosing/mixing, injection, cavity, vent/vacuum and cure controls may matter | Traceability, inspection plan, process records, reaction plan |
Use this matrix as a review framework, not a process specification. The manufacturing partner still has to convert it into an actual mold concept, process window, inspection plan, and quotation assumptions.
Compare Tooling and Part Geometry Needs
A silicone keypad is mechanically active. Thin webs create the force curve, contact features must align with the circuit, and perimeter geometry may locate or seal the assembly. The molding route therefore affects more than cosmetic shape.
For compression molding, review how the charge will be placed and how material will move as the mold closes. Large section changes, isolated pockets, tall key walls, thin webs, and inserts can influence fill and venting.
For LSR injection, review gates and runners, cavity balance, shutoff condition, venting or vacuum and the flow path to thin keypad features. Dosing, cold-runner nozzles and vacuum are available configuration features, not requirements for every keypad. Confirm which features the project needs and which equipment the proposed production line actually provides.
For either route, confirm parting line, feed or charge location, vents, flash limits, trimming method, draft/demolding, texture, shrinkage compensation, and cavity-level critical dimensions. Do not assume that a compression-mold cavity can move unchanged to LSR injection. The feed system, flow behavior, venting, thermal conditions, and process controls require a fresh tool review.
Review Contacts, Colors, and Secondary Operations
A molded keymat is often only one step in the finished HMI. Conductive contacts, legends, coatings, laser openings, lighting features, assembly, and inspection may dominate the complete process flow.
If the keypad uses carbon pills, conductive inserts, metal elements, or another molded-in feature, ask how those items will be positioned and retained. The issue is not whether one molding process is theoretically capable of using inserts; it is whether the selected route controls location, contamination, retention, and cavity-to-cavity repeatability.
For an integrated module, review the molded part with the circuit and housing. JASPER’s silicone keypad assemblies page shows why contact alignment, stack height, lighting, sealing, and electrical testing belong to one assembly-level review.
Both process families can use colored silicone with an appropriate material system. Multi-color parts may require extra molding steps, special tooling, or multi-component equipment. Printing, sprayed coatings, protective finishes, laser-opened legends, deflashing, and final optical inspection can remain secondary operations regardless of the molding route. Compare the entire manufacturing route, not only mold cycle time.
Evaluate Capacity and Quality Controls
Production capacity cannot be inferred from the process name. Output depends on the actual machine, cavity count, cure time, loading/unloading method, inserts or contacts, secondary finishing, inspection, scrap/rework rules, maintenance, and shift plan.
That is why statements such as “LSR is always for high volume” or “compression molding is only for prototypes” are poor sourcing rules. Instead, ask each supplier to define the quoted production model.
For compression molding, the control plan may need to address material preparation, charge weight/placement, cure condition, cavity identity, venting/flash, trimming, insert loading, and downstream dimensional/force/electrical inspection. For LSR injection, the plan may need to address material identity, dosing/mixing, injection and fill behavior, tool/cavity status, venting or vacuum where used, cure, handling, insert loading, and the same downstream product checks.
The exact parameters and limits belong in the manufacturing process specification. They should not be invented in a public OEM article.
Validate the Keypad, Not Just the Molding Process
A molding route is acceptable only when production-intent parts meet the complete keypad requirements. A faster cycle cannot compensate for poor tactile behavior, contact misalignment, unstable legends, light leakage, enclosure interference, or weak traceability.
The validation plan should connect the selected material and process to molded dimensions, force-displacement behavior, key return, electrical closure on the specified circuit, flash/cosmetic limits, color and finishing, backlighting where applicable, enclosure fit and preload, application-specific environmental testing, and traceable records linking material, tool revision, cavity, process route, and test method.
JASPER’s tooling and prototyping guide covers first articles and production release in more detail. This comparison should stop at the earlier decision: choosing the molding route before those approval gates are locked.
Select a Route with the Manufacturing Partner
Compression molding deserves consideration when the selected HCR system, geometry, insert/contact method, tool design, secondary operations, lot pattern, and supplier economics fit the project.
LSR injection deserves consideration when the selected LSR system, geometry, closed-mold filling strategy, automation potential, cavity plan, repeatability controls, and total production economics justify the process and tooling requirements.
Neither route should be chosen only from a generic volume label.
For a useful review, send the current 2D/3D geometry, representative key sections, circuit/contact map, enclosure CAD, target force and travel, contact/insert method, colors and surface finishes, backlighting information, environment/compliance requirements, prototype and annual quantities, typical lot size, supply boundary, and required validation records. Unknown items can be marked TBD so they are visible before tooling assumptions become expensive.
For projects ready for supplier review, start from JASPER’s custom silicone rubber keypads product family and request a keypad engineering review with the drawing package and expected production scope.
Frequently Asked Questions
Is LSR the same thing as liquid injection molding?
No. LSR is a liquid silicone rubber material family. Liquid injection molding is a processing route commonly used to meter, mix, inject, and cure LSR. Specify the material and the molding process separately.
Is HCR only used for compression molding?
No. HCR is common in compression and transfer molding, but material manufacturers also document HCR injection molding. Confirm the proposed material grade and production route rather than assuming the process from the term HCR.
Is LSR injection always cheaper for high-volume keypad production?
No. LSR can provide automation and cycle-time advantages, but total economics also depend on tooling, cavity count, insert loading, color changes, secondary finishing, inspection, scrap, maintenance, lot size, and design stability. Compare the quoted production model rather than using a universal volume threshold.
Can one keypad design move from compression molding to LSR injection without redesign?
Not safely as a general assumption. The route can change the feed system, venting, cavity balance, shutoffs, flash strategy, demolding, shrinkage behavior, insert loading, and process controls. Re-review the mold concept and critical geometry when the route changes.
Which process is better for carbon-pill contacts or multicolor keypads?
Neither process wins from the label alone. Ask how contacts or inserts are located, how colors are introduced, what secondary operations remain, and how the finished part is inspected. A faster molding step can lose its advantage if contact loading, coating, laser, trimming, or testing becomes the bottleneck.
What should an OEM compare in two supplier quotes?
Compare the material family, exact molding process, tool concept, cavity count, contact/insert method, secondary operations, traceability, quality controls, validation plan, tool ownership/maintenance assumptions, and quoted production basis. Require each supplier to identify what is included, excluded, or still TBD.
Discuss Your Tooling and Prototype Plan
Send the keypad drawing or sample, mating PCB and enclosure information, required quantities, equipment application, key feel and contact requirements, graphics/lighting needs, environment, validation expectations, and open items. Mark unknown information as TBD so the molding route can be reviewed before the production tool is fixed.
Ready to Start Your Project?
Tell us about your membrane switch, keypad, or graphic overlay requirements. Our engineering team will review your specifications and provide a detailed quote.