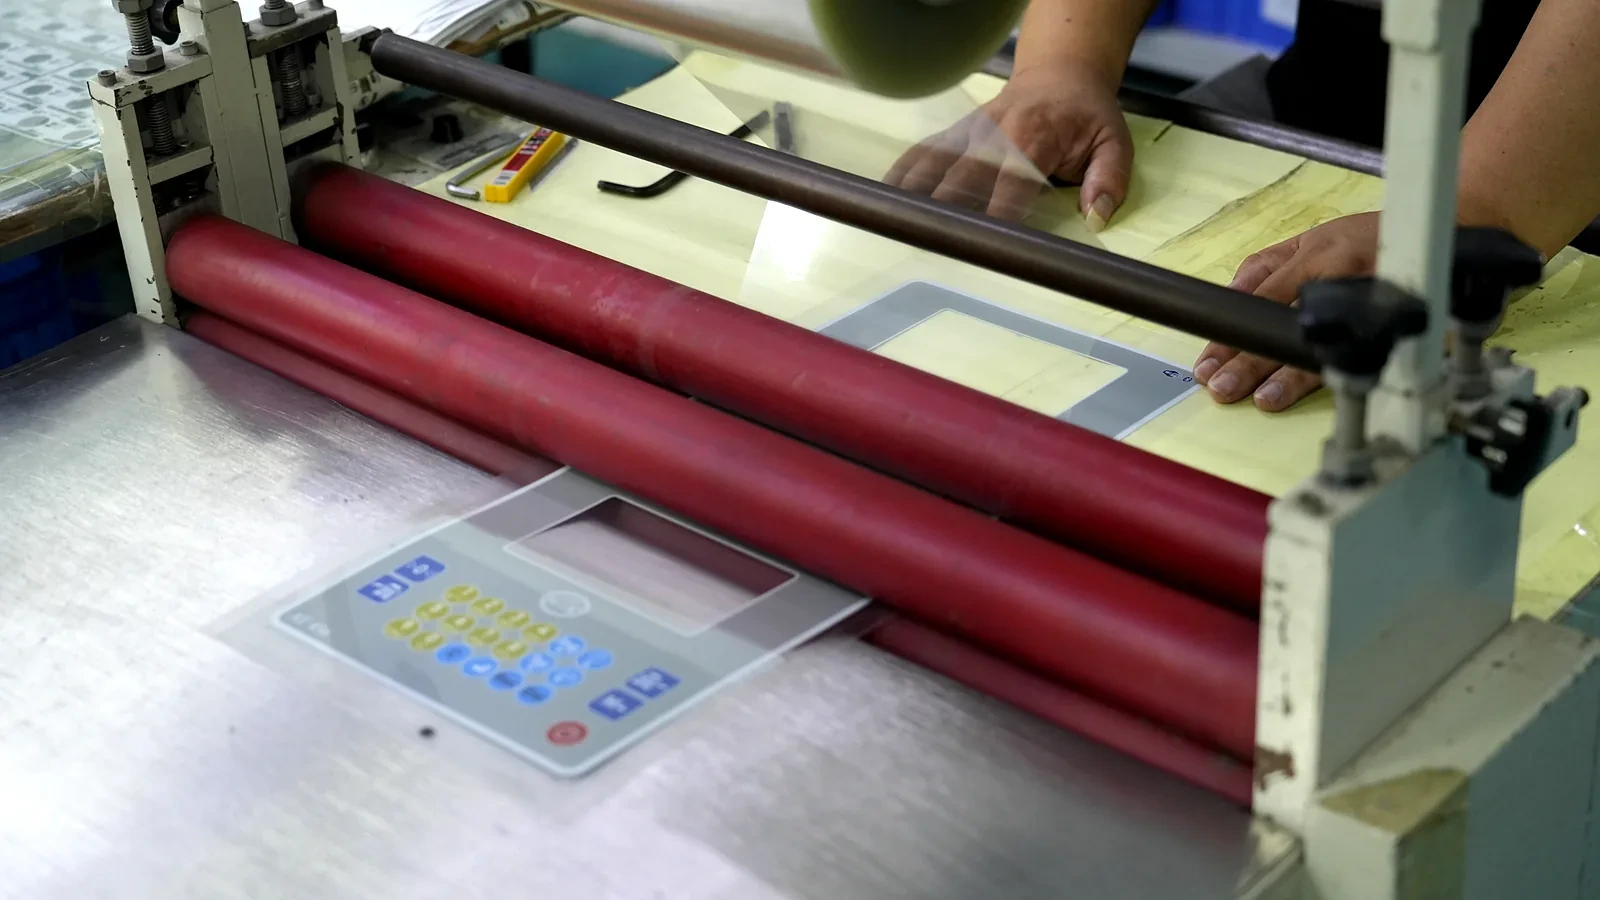
Specify membrane switches for food processing equipment from the cleaning duty at the installed panel—not from the equipment name or an IP number alone. The design review should connect what reaches the interface, how operators use it, and what the complete assembly must still do after cleaning.
When reviewing waterproof membrane switches, separate ingress protection, cleaning-chemical compatibility, cleanability, and operating performance. Use the planning tables below to define a project-specific qualification; they are not completed test records or universal acceptance specifications.
- What will reach the panel during production and cleaning?
- What belongs in a cleaning-exposure specification?
- How should glove use, visibility, and unintended inputs be checked?
- Which interfaces must be reviewed as one sealing system?
- Overlay, printing, and windows
- Perimeter, mounting surface, and housing seal
- Tail exit and rear-side interfaces
- Adhesive and installation process
- Does an IP rating establish washdown or food-contact suitability?
- How should samples be tested against the cleaning duty?
- What should the acceptance record contain?
- What should you send JASPER for a focused design review?
What will reach the panel during production and cleaning?
Start with the panel’s position and operating tasks, then describe production and cleaning as separate exposure conditions.
Illustrative example—not a JASPER customer case: Consider a portioning machine with a vertical control panel beside, rather than above, the product path. Operators select recipes, acknowledge messages, and use routine controls with approved gloves. The interface may encounter production splashes, local wiping between tasks, and an external wash during shutdown. A remote control station outside that wash area needs its own exposure record, not an assumed copy of the machine-mounted panel’s requirements.
Use a location photograph to identify the front face, lower edge, display window, mounting joint, and tail exit. Mark where fluid arrives, collects, drains, or could transfer toward food.
| Exposure mode | What to establish at this location | Design or verification question |
|---|---|---|
| Production splashes | Product residues, incidental water, splash direction, and whether controls remain in use | Can operators identify and actuate the intended key with the expected surface condition? |
| Shutdown washdown | External cleaning sequence, exposed sides, covers, equipment state, and return-to-service procedure | Which window, perimeter, housing, and tail joints receive the actual cleaning exposure? |
| Local wiping | Approved wipe and product, rubbing pattern, edge contact, and whether the interface remains powered | Does wiping affect graphics, bonding, visibility, or unintended-input behavior? |
| Cold/hot transitions | Panel and enclosure temperatures before cleaning, fluid temperature, humidity, cooling, and drying | What happens to window clarity, seals, bonds, and operation during transitions and recovery? |
Do not substitute an internal cleaning-in-place recipe for the external panel’s exposure record. Establish whether that liquid actually reaches the interface and by what route.
What belongs in a cleaning-exposure specification?
Identify the actual cleaning product and the complete application sequence. A chemical family or a statement such as “daily washdown” is not a reproducible test condition.
EHEDG’s discussion of external cleanability testing distinguishes the soiling, cleaning, and cleaning-validation stages. It also identifies nozzle selection, spray angle, and spray movement as additional variables in external cleaning. These details belong alongside chemistry and temperature in the project record.
Cleaning-exposure worksheet: field guide. Create a separate record for each panel location, cleaning step, and cleaning product. Enter the approved procedure first; during qualification, record the conditions actually applied. This table contains instructions, not assumed cleaning values.
| Field | What to enter |
|---|---|
| Location and procedure | Equipment name, panel position, cleaning-step name, procedure revision, responsible owner, and relevant food soil or residue |
| Chemical identity | Manufacturer, exact trade name, relevant active ingredients, and current product label, technical instructions, and safety data sheet |
| Concentration | Working concentration, units and basis, permitted range, and verification method; distinguish product dilution from active-ingredient concentration |
| Temperature | Cleaning-fluid temperature and panel/substrate temperature, including initial cold or hot conditions |
| Contact time | Required wet-contact period, time before rinsing where applicable, and any permitted interruption or reapplication |
| Frequency and sequence | Routine frequency, changeover or deep-clean events, order of products, and intervals between exposures |
| Application and mechanical action | Wipe or brush material and rubbing procedure; for spray, nozzle, pressure measurement location, flow, distance, angle, and movement |
| Rinsing | Whether rinsing is required by the approved procedure; water condition, application method, and duration where applicable |
| Drying and restart | Draining, wiping, air drying, or other approved method; environmental conditions and permitted return-to-service state |
| Exceptions and controls | Approved operating ranges, foreseeable deviations, temporary covers, and equipment isolation or cleaning-mode requirements |
Use the cleaning-product instructions and the plant’s approved procedure to establish these entries. This worksheet is not a recipe and does not authorize changing concentrations, mixing products, or shortening required contact times.

How should glove use, visibility, and unintended inputs be checked?
Validate the actual operator tasks with the approved gloves and expected wet-surface conditions, rather than accepting “glove compatible” as a complete requirement.
Record glove material, size range, fit, and any required layering. Have representative users select a recipe, change a setting, acknowledge an alarm, and confirm the resulting state. Check missed presses, repeated inputs, adjacent-key selection, release behavior, and whether the hand obscures a critical indicator. Include wet bare-hand operation only where the plant permits it.
Evaluate legends, indicator states, and display information from the intended viewing positions under the installation’s lighting. Repeat with the relevant surface moisture, reflections, and condensation conditions. Set readability criteria around recognizing the required information—not merely whether the backlight illuminates.
For a washdown membrane keypad, include a separate unintended-input check during permitted wiping and incidental contact. Use an instrumented bench or safe simulation to observe key events and controller responses without enabling hazardous machine movement. Human usability trials should use a safe wetting simulation; chemical exposure tests belong in a controlled test procedure.
Agree with the OEM how commands are handled during cleaning and restart. Do not treat a software cleaning screen or a membrane key as a substitute for the equipment’s approved safety and isolation measures. Choose key spacing, operating force, and window placement from the task results rather than imposing one value on every glove or machine.
Which interfaces must be reviewed as one sealing system?
Review the complete installed assembly, including the interfaces between components. Use a section drawing to make each proposed liquid barrier and exposed edge explicit.
Overlay, printing, and windows
Specify the film grade, thickness, surface treatment, print side, ink system, and relevant curing process. Distinguish a clear area within continuous film from a bonded lens or a physical opening; they require different joint reviews.
For example, MacDermid Alpha’s Autoflex EB product information describes hardcoated polyester with gloss or antiglare finishes and different ink-primer options. That illustrates why “PET overlay” is incomplete identification. The page does not establish compatibility with the cleaning sequence in your project.
Test the selected printed and converted construction, including embossed areas and cut edges. For reverse-printed designs, document how ink and bond interfaces are protected at the perimeter and openings; do not assume print location qualifies the assembly for washdown.
Perimeter, mounting surface, and housing seal
Show the mounting land, corners, recesses, bezel, gasket joint, and any fasteners. Review whether the proposed detail is accessible to the cleaning method and provides the intended drainage without exposing an unprotected bond edge.
Define the actual housing material and finish, flatness requirements, support, and gasket compression controls. Keep spacer and gasket functions distinct; the sealing, spacer, and gasket materials page provides the broader construction reference. Neither the keypad’s rear adhesive nor the enclosure gasket should be assumed to perform the other’s job without verification.
Tail exit and rear-side interfaces
Draw the tail slot, thickness transitions, sealing detail, routing, strain relief, and connector location. State which side is exposed during cleaning, including maintenance access. Check whether liquid can reach the rear through the mounting joint or tail opening even when the front face appears intact.
Where the switch construction needs a vent path, identify its protected termination and include it in the review. Do not add or block vents without checking the effect on the selected switch construction.
Adhesive and installation process
Qualify the bond on the production substrate and finish, not only on an unrelated smooth test surface. Record surface preparation, application conditions, pressure, and time before cleaning according to the selected material’s instructions. Use pressure-sensitive adhesive selection as a starting point for that review, not as a substitute for assembly testing.
The 3M 7966MWS technical data sheet provides a useful evidence-boundary example: its environmental statements are based on impervious faceplates bonded to metal, and its data are identified as typical rather than specification limits. Those statements do not qualify a finished keypad on a different enclosure. This example is not a recommendation to use that grade.
Does an IP rating establish washdown or food-contact suitability?
No. Keep enclosure ingress evidence separate from cleaning durability, operating performance, and the applicable food-contact assessment.
The official scope of IEC 60529 concerns degrees of protection provided by enclosures. For procurement, require the report to identify the tested assembly and conditions. Do not treat an IP designation as evidence that the selected detergent cycle preserves printing, adhesive bonds, readability, or key response. The waterproof membrane switch design guide covers the broader ingress-design questions; the cleaning-exposure record defines the additional project checks.
Food-equipment use also does not establish food-contact compliance. For US human-food operations subject to the relevant provisions of 21 CFR Part 117, §117.40(c) addresses cleanable non-food-contact equipment. The definition in §117.3 also includes surfaces from which drainage or other transfer to food or food-contact surfaces ordinarily occurs during normal operation. Position alone is therefore insufficient to classify the panel.
Have the OEM’s compliance team establish the intended market, exposure category, and required material documentation. Do not accept a polymer name, an antimicrobial claim, or an IP rating as a substitute for that assessment.
How should samples be tested against the cleaning duty?
Approve a written plan before testing, then move from material screening to the production-representative mounted assembly.
Begin with the specified film, ink, coating, adhesive, gasket, and housing finish. Screening coupons can help compare candidate combinations, but reserve separate samples for destructive bond measurements where needed. Record material identities and revisions so a later substitution is visible. Retain unexposed control samples under documented storage conditions for comparison.
Assemble qualification samples with the proposed mounting process, window construction, tail seal, enclosure gasket, and installation conditions. Record baseline appearance, bonding, readability, key response, and electrical behavior. Include the controller configuration when the acceptance requirement depends on how key events are interpreted.
Apply the cleaning steps in the agreed order. Include production-relevant actuation and cold/hot transitions where they form part of the duty. Inspect at planned intervals, immediately after exposure where relevant, and after a defined recovery period. A check performed only after complete drying cannot establish behavior while the interface is wet.
Choose exposure counts and sample quantities from the intended cleaning frequency, service or replacement interval, variation, and failure consequences. Document the rationale and any acceleration assumptions. Do not convert a more concentrated solution, a hotter test, or a brief immersion result into an unsupported service-life claim.
Keep surviving cleaning separate from being effectively cleaned. For the latter, the plant hygiene team should define representative soils, difficult-to-clean locations, residue assessment, and any necessary hygiene validation. Appearance alone is not the acceptance method for every hygiene requirement. EHEDG’s separation of soiling, cleaning, and validation is useful here; the project plan should not be represented as an EHEDG certification test.
Agree which checks belong to the component supplier, OEM, plant, or an external laboratory. Use project-specific testing and quality control to frame that discussion, not as evidence that a particular food-equipment assembly has already passed.
What should the acceptance record contain?
Link every requirement to a sample method, an agreed acceptance criterion, and retained evidence. Keep appearance, adhesion, readability, operating feel, and electrical results separate rather than combining them into “passed cleaning.”
Requirement-to-test planning matrix. The entries below describe proposed checks. Complete the project’s limits and approval responsibilities before testing; the table reports no test results.
| Requirement | Proposed sample check | Acceptance definition to agree | Evidence to retain |
|---|---|---|---|
| Appearance and surface integrity | Compare the same areas before and after exposure, including embossing and cut edges | Permitted cosmetic changes; rejection rules for cracking, blistering, exposed print, or material shedding | Matched photographs, inspection conditions, defect locations |
| Adhesion and joint integrity | Inspect perimeter and window bonds; perform defined bond tests on representative assemblies or companion coupons | Edge-lift and bond-strength limits; measurement method, recovery time, and unacceptable failure modes | Edge measurements, bond-test method/results, failure-mode photographs |
| Readability | Identify required legends, values, and indicator states at approved viewing positions in relevant wet and dry conditions | Required information remains distinguishable under the specified lighting and surface conditions | Task results, lighting and viewing setup, photographs |
| Operating feel and release | Repeat the glove-task script; measure force/displacement when part of the requirement | Approved response range and release behavior; limits on missed or repeated operation | Glove details, observations, measurements where specified |
| Electrical and command behavior | Log intended and unintended key events; check specified circuit properties under relevant conditions | Drawing and controller limits; agreed rejection rules for opens, shorts, unintended commands, or failed release | Circuit results, event logs, controller revision, test conditions |
| Ingress and mounting integrity | Evaluate the complete mounted configuration using the selected ingress method and agreed cleaning preconditioning | Acceptance criteria from the specified method plus separately defined assembly requirements | Report identifying the enclosure, seals, mounting process, and preconditioning |
| Cleanability and residue control | Assess selected soils and difficult locations using the plant-approved method | Residue and hygiene criteria established by the responsible hygiene team | Method, inspection or sampling locations, results, approvals |
Give each requirement an identifier. Each test record should connect that identifier to the sample, material and drawing revisions, cleaning-procedure revision, actual exposure, inspection timing, result, deviations, and disposition. Maintain a visible link between the requirement and the evidence rather than retaining only a final pass/fail summary.
Review the qualification when a cleaner, dilution range, temperature, overlay construction, adhesive, housing finish, seal detail, or relevant controller behavior changes. Decide which evidence remains applicable and which checks need repeating.
What should you send JASPER for a focused design review?
Send the equipment location, cleaning procedure, and interface drawings together. These inputs define what the food equipment control panel must withstand and which parts of the assembly need review.
- Equipment and location photographs: identify the machine and operator tasks; show the overall installation, panel perimeter, window, rear mounting, and tail exit. Mark splash and cleaning directions where known.
- The actual cleaning procedure: include exact products, working concentrations, temperatures, contact times, frequency, application method, rinsing, drying, and permitted equipment state. Attach the relevant product instructions.
- Panel and interface drawings: include dimensions, artwork, key and window layout, mounting surface and finish, gasket or seal details, tail routing, connector, and electrical pinout. Add glove requirements and existing acceptance criteria.
Send your food-equipment interface requirements for a project-specific discussion of the keypad construction, mounting interfaces, and proposed sample checks. Define the review boundary explicitly: interface-component evaluation does not, by itself, establish the complete machine’s washdown performance, hygienic suitability, or regulatory compliance.
Ready to Start Your Project?
Tell us about your membrane switch, keypad, or graphic overlay requirements. Our engineering team will review your specifications and provide a detailed quote.