Cleaning chemicals attack graphic overlay materials by softening the topcoat, leaching plasticizers, or crazing the polymer backbone. Polyester (PET) survives most hospital-grade disinfectants. Polycarbonate (PC) fails fast against bleach, accelerated H₂O₂, and high-pH quats unless protected by a chemically resistant hardcoat.
- 1. The Real Stress: Why Cleaning Chemicals Reach Graphic Overlay Materials First
- 2. How Cleaning Chemicals Attack the Overlay Stack — Five Failure Modes
- 3. Material × Chemical Compatibility Matrix
- 4. The Standards Behind the Numbers — ASTM D543 and ISO 175
- 5. What Chemical-Compatibility Data to Request from an Overlay Supplier (RFQ Checklist)
1. The Real Stress: Why Cleaning Chemicals Reach Graphic Overlay Materials First
A medical infusion pump survives 500,000 actuations, but that does not establish overlay cleaning life. This example uses disinfectant wipes 30 times per shift, around 22,000 chemical exposures per year. The roughly 600 healthcare-surface formulations cited in the CDC/EPA context do not establish compatibility with thermoplastic substrates.
Food-equipment OEMs face the same arithmetic from a different angle. FDA 21 CFR 175.300 governs resinous coatings that contact food directly, but the operator panel on a commercial mixer or a sous-vide bath is wiped 8 to 15 times per shift with peracetic acid at 0.2 % or quaternary ammonium at 200–400 ppm. ISO 11607-1:2019 — written for sterile packaging — applies the same principle the OEM overlooks: any wetted polymeric surface in a repeat-cleaning environment must be specified against the actual cleaning agent, not “chemical resistance” as a generic line item.
The result is a recurring field-failure pattern. Graphic overlay materials fade, craze, haze, or delaminate not because the polymer was wrong in absolute terms, but because the cleaning protocol the end user adopted in year three was never on the original specification sheet. The fix begins with knowing how each chemical actually attacks the stack.
2. How Cleaning Chemicals Attack the Overlay Stack — Five Failure Modes
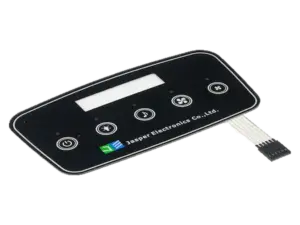
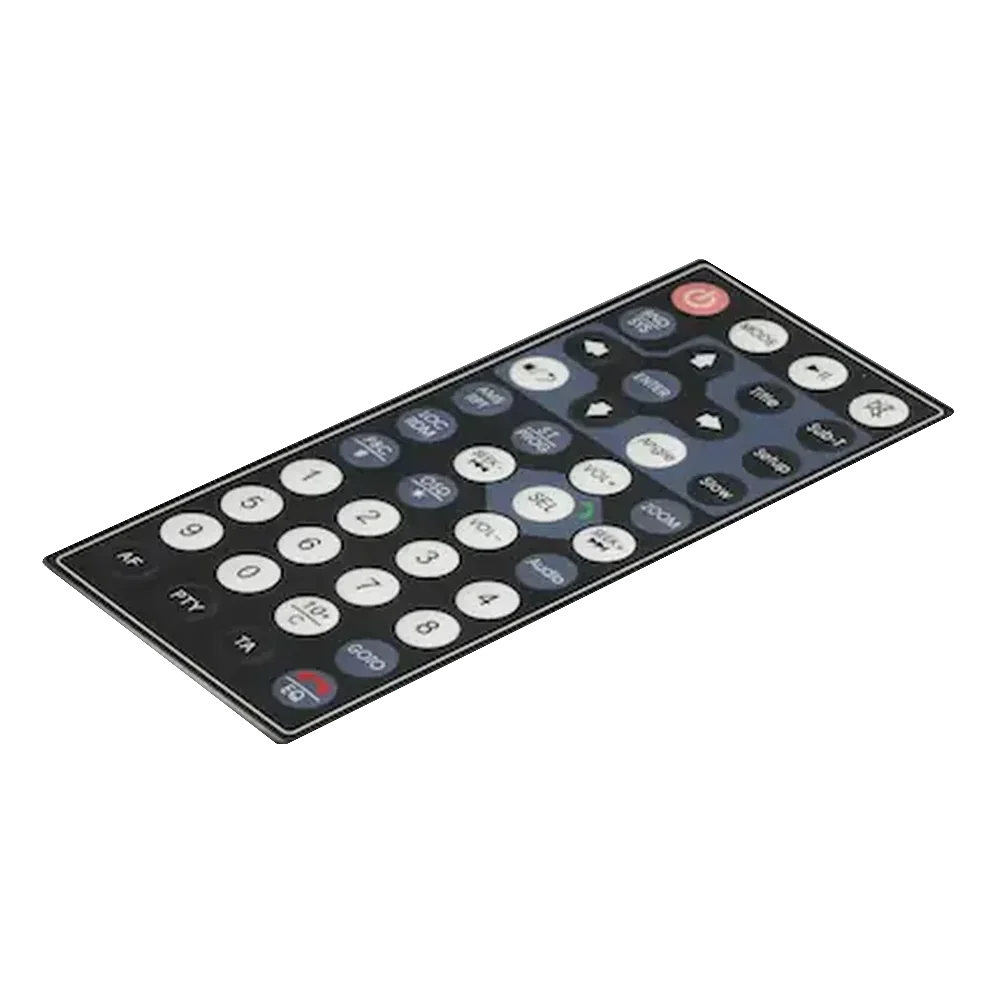
A graphic overlay is a five-layer sandwich: hardcoat, base film (PET, PC, PMMA, PVF, or PEN), printed ink layer, optional adhesive primer, and pressure-sensitive adhesive (PSA) on the bottom. Cleaning chemicals attack one or more of these layers through five distinct mechanisms. Each mechanism has a visible signature, which is the engineer’s diagnostic shortcut when an overlay fails in the field.
Solvent crazing is a common polycarbonate failure. Fine surface cracks can appear within 24–72 hours of repeated exposure to ketones such as acetone or MEK, aromatic alcohols, or concentrated ethanol, propagating from stress concentrations at die-cut edges. For the Makrofol DE example, acetone, MEK, and methylene chloride are classified as incompatible at any concentration.
Plasticizer migration affects PVC overlays and some printed ink formulations. Disinfectants containing surfactants or alcohols pull plasticizer to the surface, creating a tacky film that traps dirt and reads as “the overlay got sticky” in service reports. PET and PC are unplasticized and immune; PVC overlays should be avoided in any chemically active environment.
Hardcoat hazing can follow oxidation of an acrylic or silicone coating under repeated bleach or peracetic-acid exposure. The comparison describes a 5–15 % loss of optical transmission over six months: the overlay may still function while backlit icons lose contrast and fail the OEM’s visual acceptance criteria. The coating example compares untreated PC at 2H pencil hardness with silicone-hardcoated PC at 4H–6H and associates the harder coating with better chemical resistance. Confirm the actual coating and chemical exposure; pencil hardness alone is not a chemical-compatibility test.
Ink leaching happens when subsurface inks are not fully encapsulated by the base film. Alcohol-based disinfectants seep through any pinhole in the topcoat and lift pigment. The pattern is unmistakable: a faded halo around the most-pressed keys, where wipe contact concentrates. Subsurface (second-surface) printing is the standard defense and is required on any overlay rated for medical disinfection.
Adhesive softening and edge lift occur at layer interfaces. Cleaning fluid can reach the bottom PSA through cutouts and die-cut edges, so include that exposure in testing. Review the chemical-compatibility data for the exact adhesive, such as 467MP, 9485PC, or 4965, before field use rather than after a return.
3. Material × Chemical Compatibility Matrix
The matrix compares five overlay materials against eight cleaning formulations using published grade data and available ASTM D543 immersion data. The source grades include Melinex, Tedlar, Makrofol, Lexan, and Acrylite. C means compatible: no visible change after 1,000 wipes or 7-day immersion. Co means conditional on hardcoat or limited frequency. X means incompatible, with visible damage in days rather than months. These ratings do not qualify an untested formulation or finished assembly.
| Cleaning chemical | PET (e.g., Melinex) | PC (Makrofol DE, Lexan 8010MC) | PC + silicone hardcoat | PMMA (Acrylite) | PVF (Tedlar) | PEN (Teonex) |
|---|---|---|---|---|---|---|
| 70 % Isopropyl alcohol (IPA) | C | Co | C | C | C | C |
| 99 % IPA | C | X (crazing) | Co | Co | C | C |
| 70 % Ethanol | C | Co | C | C | C | C |
| 17 % IPA + quaternary-ammonium formulation | C | Co | C | Co | C | C |
| 55 % IPA + quaternary-ammonium wipe formulation | C | X | Co | Co | C | C |
| Quaternary-ammonium formulation (II 256 example) | C | Co | C | C | C | C |
| Accelerated H₂O₂ 0.5 % formulation | C | Co | C | Co | C | C |
| 10 % household bleach (≈ 0.5 % NaOCl) | C | X (yellowing, crazing) | Co | X | C | C |
| Peracetic acid 0.2 % formulation | C | X | Co | X | C | C |
| Quaternary ammonium 200–400 ppm | C | C | C | C | C | C |
| Acetone, MEK (reference: industrial degreaser) | Co | X | X | X | C | C |
A few patterns are worth noting. PET is the broadest-spectrum substrate; it tolerates the full hospital disinfectant range and most food-grade cleaners at the concentrations actually used in service. Unhardcoated PC is the highest-risk choice for any wipe-down protocol involving bleach, peracetic acid, or 99 % IPA — three of the most common chemicals deployed against drug-resistant pathogens and food-borne contamination. PC with a properly specified silicone hardcoat closes most of that gap, but it does not match PET against neat bleach. PVF (Tedlar) is the niche specialist for aggressive industrial chemicals; it dominates aerospace and military panels for the same reason. PEN sits between PET and PVF in chemical performance and adds high-temperature stability above PET’s 120 °C ceiling.
The matrix has limits. It reflects topcoat compatibility, not full-stack lifetime. Ink, hardcoat, and adhesive layers each carry their own ratings, which is why the §5 RFQ checklist below asks for them line by line.
4. The Standards Behind the Numbers — ASTM D543 and ISO 175
Two test standards underpin every credible compatibility claim. Without a named test method and a stated exposure regime, “chemical resistant graphic overlay” is marketing language, not engineering data.
ASTM D543-21 “Standard Practice for Evaluating the Resistance of Plastics to Chemical Reagents” defines two procedures. Practice A is full immersion: a coupon of the candidate material sits in the reagent for 7 days at 23 °C. Practice B is variable exposure under load or stress. After exposure the coupon is rinsed, dried, and measured for mass change, dimensional change, tensile strength change, and visual appearance. ASTM publishes a reference list of 50 reagents; cleaning-chemical compatibility tests usually substitute the named end-user disinfectant for the closest analog on the list.
ISO 175:2010 “Plastics — Methods of test for the determination of the effects of immersion in liquid chemicals” is the international equivalent. Same coupon principle, same exposure measurements. ISO 175 is more commonly cited on European TDSes; ASTM D543 dominates North American suppliers. Either is acceptable; the failure is when the supplier names neither.
A third method is rising in medical-device work. ISO 22196 covers antimicrobial efficacy on surfaces and is increasingly bundled with chemical-compatibility data for repeat-disinfection contexts. ISO 11607-1:2019, written for sterile barrier packaging, requires demonstration that the material maintains specified properties through the validated cleaning and sterilisation regimen — which in practice means an ASTM D543 or ISO 175 report on the actual disinfectant used.
Pass/fail thresholds vary by application. For medical overlays the typical threshold is ≤ 2 % mass change, no visible crazing, and no tactile change after 1,000 wipe cycles or equivalent immersion. Food-equipment OEMs tend to use the same 2 % threshold with peracetic acid as the worst-case reagent. The threshold should appear on the overlay drawing, not in an email.
5. What Chemical-Compatibility Data to Request from an Overlay Supplier (RFQ Checklist)
A complete chemical-compatibility RFQ to a graphic overlay supplier should request the seven data points below. Each maps to a specific failure mode in §2 and a specific row in the §3 matrix. A supplier that cannot deliver these in 5 business days is unlikely to have done the testing.
| # | Data point | Why it matters | Acceptable evidence |
|---|---|---|---|
| 1 | Base film grade and supplier (e.g., Melinex 339, Makrofol DE 1-1 CC2) | Generic “polyester” is not a specification; grades vary in coating, gauge, and additives | Manufacturer TDS PDF |
| 2 | Hardcoat chemistry (silicone, acrylic, urethane) and pencil hardness | Hardcoat type, not just presence, drives bleach and peracetic-acid resistance | Hardcoat supplier’s certificate; ASTM D3363 pencil hardness report |
| 3 | ASTM D543 or ISO 175 test report for each named cleaning chemical | The single most-skipped document; without it, compatibility is conjecture | Lab report with method, reagent, exposure time, mass-change, visual notes |
| 4 | Ink chemistry and subsurface print confirmation | Subsurface printing is the line between “still legible” and “wiped off in 60 days” | Drawing callout + ink supplier TDS |
| 5 | PSA grade and chemical-resistance class (e.g., 467MP, 4965) | Chemical attack at die-cut edges is the underrated failure mode | PSA supplier TDS with chemical table |
| 6 | Wipe-cycle test data (typical: 1,000 cycles with named wipe) | Closer to real-world stress than 7-day immersion | In-house or third-party report with weights, photos |
| 7 | Antimicrobial / sterilisation compatibility (if medical) — ISO 22196 or ISO 11607 reference | Required by quality audit; should not surface for the first time during 510(k) review | Test report or material declaration |
For medical-device work the RFQ should also reference the supplier’s ISO 13485 certificate by number and audit body. For food-equipment work, request FDA 21 CFR 175.300 conformance documentation for any ink or coating that could migrate to a food-adjacent surface. Both documents are public; a credible supplier publishes them on request without redaction.
6. Frequently Asked Questions
Which graphic overlay material resists isopropyl alcohol best?
In the compared Melinex PET data, 70 % and 99 % IPA cause no measurable mass change after 1,000 wipe cycles. The compared PC tolerates 70 % IPA but crazes with repeated 99 % IPA contact unless protected by a silicone hardcoat. The PVF and PEN examples also pass, at higher cost. Apply these results only within the stated material and test conditions.
Can polycarbonate overlays survive hospital-grade disinfectants?
In this comparison, unhardcoated PC deteriorates under bleach, accelerated H₂O₂, the 55 % IPA/quaternary-ammonium wipe formulation, and peracetic acid, typically within 30–90 days of routine wiping. A properly specified silicone hardcoat improves PC compatibility with the compared hospital cleaners except concentrated bleach. For primary bleach or peracetic-acid exposure, PET or PVF is favored here; qualify the actual formulation and assembly.
What chemical compatibility data should I ask my overlay supplier for?
Request seven items: base film grade and TDS; hardcoat chemistry and pencil hardness; ASTM D543 or ISO 175 report for each named cleaning chemical; ink chemistry and subsurface print confirmation; PSA grade and chemical-resistance class; wipe-cycle test data (typically 1,000 cycles); and ISO 22196 or ISO 11607 documentation for medical use. The full checklist is in §5 above.
Is ASTM D543 or ISO 175 the right test method for cleaning-chemical exposure?
Either is acceptable. ASTM D543-21 dominates North American supplier TDSes; ISO 175:2010 is the European equivalent. Both define 7-day immersion and quantify mass, dimensional, and visual change. For wipe-down scenarios, supplement with a 1,000-cycle wipe test using the actual end-user wipe — immersion alone overestimates fluid contact time.
Why does polycarbonate craze when wiped with bleach?
Sodium hypochlorite can oxidise the carbonate backbone and residual bisphenol A, creating local stress and fine cracks. The reaction accelerates at die-cut edges with high molecular alignment. In the Makrofol DE example, NaOCl solutions at 5 % or above are classified as incompatible without hardcoat protection.
Do hardcoats make polycarbonate equivalent to polyester for chemical resistance?
No, but they close most of the gap. A 4H–6H silicone hardcoat on PC matches PET against IPA, ethanol, and most quaternary-ammonium disinfectants. It does not match PET against neat bleach (NaOCl ≥ 5 %) or concentrated peracetic acid. For those reagents, specify PET or PVF instead of relying on a hardcoat.
How many wipes with the compared 17 % IPA/quaternary-ammonium formulation can PET withstand?
The cited PET example, with silicone hardcoat and subsurface printing, exceeds 5,000 wipes with the 17 % IPA/quaternary-ammonium formulation before measurable optical change, described as roughly five years at 3 wipes per shift. This is formulation-specific, not a universal wipe-life rating. Adhesive edge lift, rather than topcoat damage, is the typical end-of-life mode in the example; confirm the PSA against the same chemical.
What is the safest overlay material specification for food-contact-adjacent equipment?
Polyester (PET) base film with a silicone hardcoat, fully subsurface-printed inks compliant with FDA 21 CFR 175.300 for any food-adjacent migration path, and a PSA rated against peracetic acid 0.2 % and quaternary ammonium 400 ppm. PVF is an upgrade for direct washdown environments. Avoid PVC and unhardcoated PC for any food-equipment overlay.
Disclosure: This explainer was authored by JASPER Electronics, a custom graphic overlay and membrane switch manufacturer. The technical content above is vendor-neutral and applies to any compliant supplier.
Ready to Start Your Project?
Tell us about your membrane switch, keypad, or graphic overlay requirements. Our engineering team will review your specifications and provide a detailed quote.