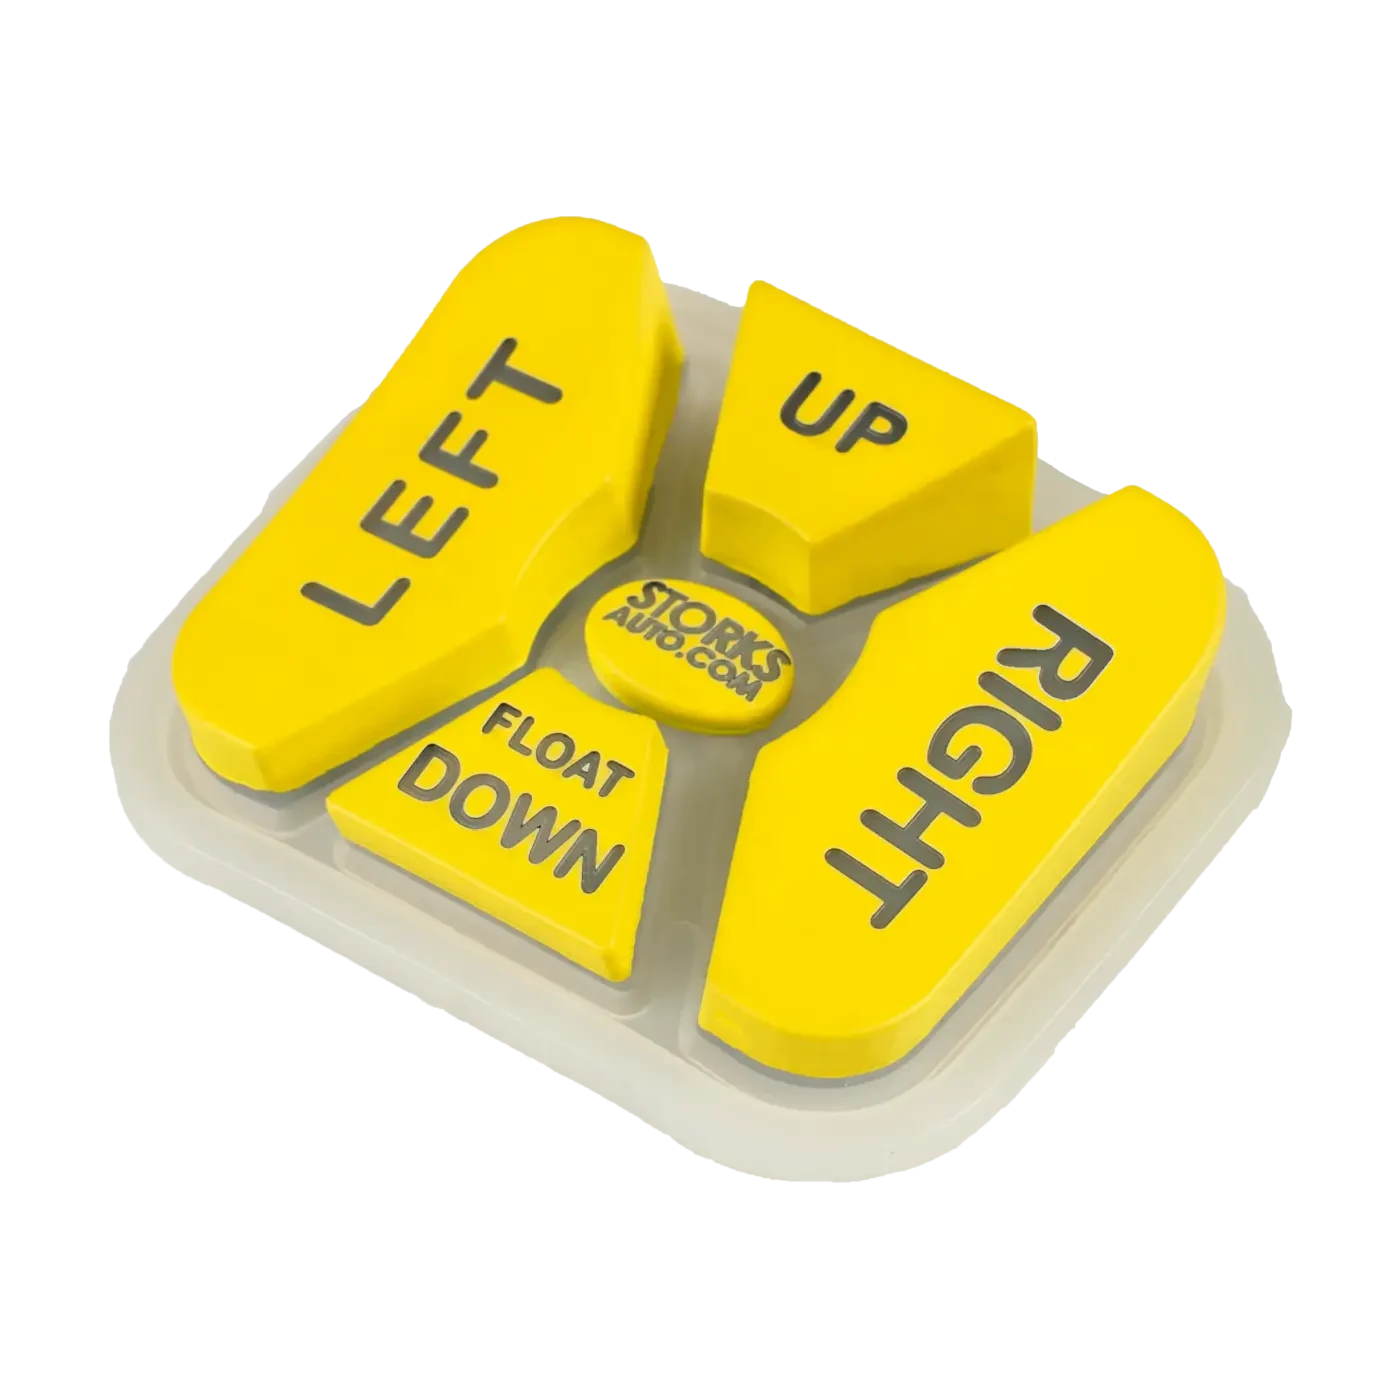
Silicone keypads are made by molding and curing a silicone compound, then completing the contacts, surface finishing and assembly operations required by the design. Compression molding is one option, not the only silicone keypad manufacturing process. S1 A useful production plan connects the selected route to checks and records that show what was made, how it was inspected and who authorized its release.
For OEM buyers, the practical question is not simply “How are silicone keypads made?” It is “Which operations are included in this order, and what evidence follows the parts?” The framework below is a proposed purchasing and process-control starting point, not a universal manufacturing specification.
- 1. Release the Design and Manufacturing Scope
- An illustrative, owner-tagged manufacturing flow
- 2. Prepare Tooling and Approved Materials
- 3. Mold and Inspect the Rubber Part
- 4. Apply Contacts, Decoration or Coatings as Specified
- Put the contact operation in its correct place
- Control each selected surface operation
- 5. Assemble and Test Supplied Components
- 6. Control Lots, Revisions and Shipment Approval
- A Process–Input–QC–Record Table for the Purchase Specification
- Discuss Your Tooling and Prototype Plan
1. Release the Design and Manufacturing Scope
Identify the purchased item first: a molded keymat, a decorated contact-bearing part, or a tested module. Review custom silicone rubber keypads against that boundary rather than assuming every quotation includes electronics and final assembly.
The work order should reference the released drawing, bill of materials, artwork and inspection instructions. Assign an execution site and acceptance owner to every selected operation, including purchased components and returned subcontract work.
JASPER’s public product page describes compression-molded and LSR-molded builds. Its linked brochure presents process descriptions and equipment photographs. Those are public capability descriptions, not confirmation that every depicted operation is performed in-house for a particular order. A project-specific make/buy agreement should identify the actual route. J3 J6
An illustrative, owner-tagged manufacturing flow
Illustrative example: J = verified JASPER operation; P = identified, approved partner; U = ownership not established for the order. This example uses U rather than inventing factory assignments. Optional steps apply only when specified.
[U] Released work order and operation responsibilities
                         |
[U] Accepted material lots and production-ready tool
    + approved inserts, when contacts are co-molded
                         |
[U] Selected molding route and cure -> demolding
                         |
[U] Trimming / post-cure / conditioning as the route requires
                         |
[U] Molded-part acceptance
                         |
[U] Specified later contact, printing, coating or laser operations
                         |
            +------------+----------------+
            |                             |
[U] Component-only release      [U] Supplied assembly and test
            |                             |
            +------------+----------------+
                         |
[U] Lot disposition -> protective packing -> shipment approval
A failed gate should lead to identified hold stock and an authorized disposition—not an undocumented shortcut to the next operation. Reworked parts must re-enter at the checks affected by the rework.
2. Prepare Tooling and Approved Materials
Tool approval is a separate topic; use the tooling and prototyping guide for development decisions. Production preparation should instead confirm that the correct released tool, cavity configuration and operating instructions are available.
The molding route determines which process variables need control. Compression, transfer and injection molding are distinct routes; injection processes can use suitably formulated high-consistency rubber (HCR) or liquid silicone rubber (LSR). Specify the selected material and process rather than treating all silicone molding as one method.
| Industry route | How material reaches the cavity | Questions for the production plan |
|---|---|---|
| Compression | A charge is placed into the mold before closure | How are charge quantity, placement and insert loading checked? |
| Transfer | Material moves from a transfer chamber into the cavity | How are feed condition and insert location controlled? |
| Injection | A feed system delivers material into a closed mold | Which HCR or LSR system is selected, and which feed or metering checks apply? |
These are industry options, not a JASPER equipment inventory. S1
For materials, link received lots to the released specification. When mixing is included, record the approved formulation and component lots. When prepared compound is purchased, preserve its supplier identity rather than implying that every keypad manufacturer compounds its own material.
At setup, check tool condition, cleanliness, fixtures and measurement equipment status. Record the actual setup against the approved operating window; a copied recipe alone does not document what ran.
3. Mold and Inspect the Rubber Part
Separate process evidence from part evidence. Process records should identify the run, tool, material and relevant settings. Part inspection should establish whether the resulting pieces meet the requirements; neither record should be substituted for the other.
Inspect molded parts before adding the cost of decoration. A proposed gate should cover incomplete fill, trapped-air defects, contamination, damaged webs, misplaced inserts and unacceptable flash. For functional areas, describe prohibited intrusion or damage on the drawing rather than accepting every edge that looks visually tidy.
Preserve cavity and production-interval identity where relevant. Comparing only pooled results can conceal that one cavity or one interval differs from the rest. Specify how samples represent the run and what happens after a restart or adjustment.
Post-curing is not required for every silicone grade. Determine the need from the selected material and application, then document any required treatment and the condition in which measurements are taken. Do not borrow an oven cycle from an unrelated grade.
For dimensional and force checks, agree on part conditioning, support and measurement method before comparing batches. Keep trimming and handling instructions tied to the same acceptance requirements.
4. Apply Contacts, Decoration or Coatings as Specified
Put the contact operation in its correct place
A molded-in conductive pill belongs upstream of the molding step, while a qualified conductive printed region is a later operation. A silicone actuator working over a separate dome or switch follows a different assembly route. Do not combine these architectures into one compulsory production sequence. J2
Specify contact identity, position, exposed condition and the applicable retention or functional check. A statement that a conductive material was supplied is not the same as acceptance of the completed switching interface.
Control each selected surface operation
Printing needs a defined substrate, ink system and processing instruction. A silicone-ink manufacturer’s technical sheet, for example, specifies mixing and working-life controls and calls for application trials. That supports qualifying the actual material pairing—not prescribing that ink, its recipe or its performance for every keypad. S3
For a coated, laser-opened design, define the intended layer sequence and the layer to be exposed. JASPER’s existing legend guide addresses that surface-system design; the production task here is to retain the batch, artwork, treatment and inspection records for the selected construction. J7
Inspect registration, coverage and visible defects at the appropriate transfer point. Agree separately on adhesion, flexing, wear and cleaner-exposure checks, including their frequency. A visual approval should not be reported as a durability result.
For outsourced finishing, require the returning lot to retain its original identity, finishing batch reference and acceptance status. A subcontract delivery note alone should not authorize the next operation.
5. Assemble and Test Supplied Components
For silicone keypad assemblies, confirm which circuits, contacts, LEDs, spacers and connectors are actually included. The public product page lists possible assembly elements; the order must select the delivered configuration. J4
Before assembly, reconcile component part numbers and revisions. Document the fixture, locating features, fastening or bonding instructions and test configuration. Verify the output against the supplied boundary: key actuation and release, electrical connections, required contact measurements and powered lighting where included.
Define what an electrical record measures. State the circuit, sensing points and actuation condition; do not label an end-to-end reading as contact-only resistance without separating the other contributions.
Check the tester as well as the product. Specify fixture verification and the response to a failed reference check. Passing parts through a tester does not establish that the tester could detect the relevant fault.
Component inspection should not be presented as approval of customer-owned enclosure features or the completed device. Keep those acceptance responsibilities explicit.
6. Control Lots, Revisions and Shipment Approval
Use a job traveler: the record that accompanies a production lot through its operations. Link the final lot to material batches, applicable cavity identity, finishing batches, component revisions and inspection results. Record splits and merges so traceability survives subcontracting and assembly.
Separate three decisions: whether the process may continue, whether a lot is acceptable, and whether qualification evidence supports the design. NIST explains acceptance sampling as a decision about accepting or rejecting a lot, not a way to establish its exact quality level. S4
Specify which characteristics receive individual screening, which use an agreed sampling plan and which require qualification or periodic testing. State sampling rules, limits and escalation before inspection; do not keep drawing new samples until a rejected lot passes.
For an abnormal result, identify potentially affected output, including the relevant interval since the last accepted check. Segregate it, investigate the scope and document authorized rework, rejection or concession. Check other linked lots when the suspected cause extends beyond the immediate batch.
Shipment approval should reconcile accepted quantity, revision, outstanding holds, required reports and packaging. Select packaging that protects the specified surfaces and contact areas without imposing unapproved deformation. Record the authorized release rather than treating a packing label as proof of acceptance.
A Process–Input–QC–Record Table for the Purchase Specification
Illustrative control-plan template: these are proposed checkpoints, not JASPER test results. For every applicable row, assign a named owner, method, limits, frequency and failure response. No universal tolerances or sample sizes are implied.
| Operation | Required inputs | Check before transfer | Record to retain |
|---|---|---|---|
| Order release | Drawing, bill of materials, artwork, supply boundary | Revisions agree; ownership assigned | Work order and operation scope |
| Material preparation | Released material specification and identified lots | Identity, storage status, preparation instruction | Receiving and mixing records, where applicable |
| Tool setup | Released tool, cavity configuration, operating window | Tool condition, correct setup, equipment status | Setup record and restart authorization |
| Molding and insert integration | Accepted material; specified inserts | Molded defects, insert condition, process deviations | Run log, cavity/interval reference, hold record |
| Trimming and required treatment | Molded lot; approved route | Functional edges, damage, treatment completion, measurement state | Finishing/treatment record and molded-part inspection |
| Later contacts and decoration | Accepted parts; selected materials and artwork | Position, coverage, specified adhesion or electrical checks | Contact/finish batch, artwork revision, results |
| Supplied assembly and test | Released component revisions and fixture | Assembly identity, required mechanical/electrical/lighting functions | Component genealogy, fixture ID, test record |
| Final inspection and shipment | Completed traveler and packaging instruction | Lot decision, quantity, labels, holds, protective packing | Disposition, packing record and shipment authorization |
Keep the result and its meaning together. An inspection record should identify the characteristic, measured value or observed defect, unit where relevant, requirement reference and disposition. A single “QC passed” entry cannot explain which checks were performed.
Frequently Asked Questions
Should every drawing dimension be checked on every part?
Not automatically. Agree on inspection coverage according to feature risk and measurement practicality. Keep dimensional sampling separate from any individually screened functional requirements; document both in the control plan.
Can an approved color sample replace finishing records?
No. Use it as an appearance reference, while retaining material, artwork and processing identity. Otherwise, a later change cannot be connected reliably to the condition that was accepted.
Can a finishing subcontractor substitute an equivalent coating?
Only through the agreed change process. Request the proposed material, reason, affected requirements and verification evidence before accepting the substitution. A matching color alone is not sufficient justification.
Does 100% functional testing prove service life?
No. Testing every shipped unit for selected present-time functions does not test future wear or environmental exposure. Define service-life evidence separately, including the test configuration and failure criteria.
Which records should arrive with each shipment?
Agree this in the purchase specification. A practical package identifies part revision, lot, quantity, required inspection results and authorized deviations. Also define which underlying records are retained and retrievable rather than automatically shipped.
Discuss Your Tooling and Prototype Plan
Start with the drawing or sample, intended equipment, prototype quantity and expected production volume. Include the contact architecture, target key behavior, artwork, coating or lighting requirements, mating circuit and enclosure information, and the boundary of supply.
State critical acceptance requirements, documentation needs and any restrictions on subcontracting. Mark unresolved choices as TBD rather than selecting unsupported values.
Request a keypad engineering review and ask for the proposed manufacturing route, operation ownership, inspection plan and evidence package to be addressed alongside the tooling and prototype plan.
Ready to Start Your Project?
Tell us about your membrane switch, keypad, or graphic overlay requirements. Our engineering team will review your specifications and provide a detailed quote.